COSHH – Pennine Lubricants – Ultrasol X-777
This coolant is used to lubricate cutting tools and wash chips from the work area in our two CNC machines -the lathe and the mill.
Students are not expected to replenish coolant in either machine, please ask a member of technical staff to help you with this.
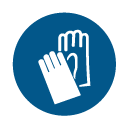
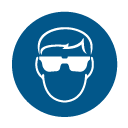
Required PPE
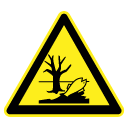
Hazards
Usage Information
Reading the refractometer
This coolant concentrate has a refractometer adjustment factor of 1.3. You must multiply the percentage value you get from the refractometer scale by 1.3 in order to arrive at the actual value.
Filling a machine with fresh coolant
You need to aim for a concentration around 6%.
Fill the coolant bucket up to the shadow line, and add 600ml of coolant concentrate. Mix gently with the mixing paddle in a combi drill set to slow speed (gearbox setting 1). This will give you approximately 5.85% strength mixed coolant.
Adding concentrate to a machine that is running low
Machines will lose coolant through chip take-out and from evaporative loss, especially during the summer months. Because the water content of the coolant can evaporate leaving the concentrate behind, we can’t just top up with normal strength coolant because we would overshoot our target value.
Instead, add coolant at a low strength – 1-2% – and regularly check the concentration of the coolant in the tank as you go. It helps to run the coolant through the machine at the same time to thoroughly mix the coolant into the existing coolant in the tank. Adjust the concentration of the coolant you are adding to achieve your target of 6%.
Adding 100ml of coolant concentration to a bucket of water filled up to the shadow line will give approximately 1% mix. This is the minimum amount of concentrate that should be used. Mix gently with the mixing paddle in a combi drill set to slow speed (gearbox setting 1).
Do not add water to the coolant tank without any coolant concentrate. Water by itself will not emulsify with the oil in the coolant properly.
The water in the area is naturally low in dissolved solids, so we don’t need to worry too much about using distilled water for making up the top-up. Keep an eye on this though, and if the coolant starts to foam excessively then it might be time to start thinking about a refresh.